Weifang, China, October 29th, 2026, FinanceWire
Bene Bags, a recognized leader in the global bag manufacturing industry, has officially announced the expansion of its custom tote bag manufacturing services, offering enhanced material selections, expanded color customization, and specialized design capabilities for corporate clients worldwide. Serving diverse sectors including retail, promotional marketing, creative agencies, and non-profit organizations, the company delivers tailored packaging and branding solutions that meet evolving global demands for sustainability and brand distinction.
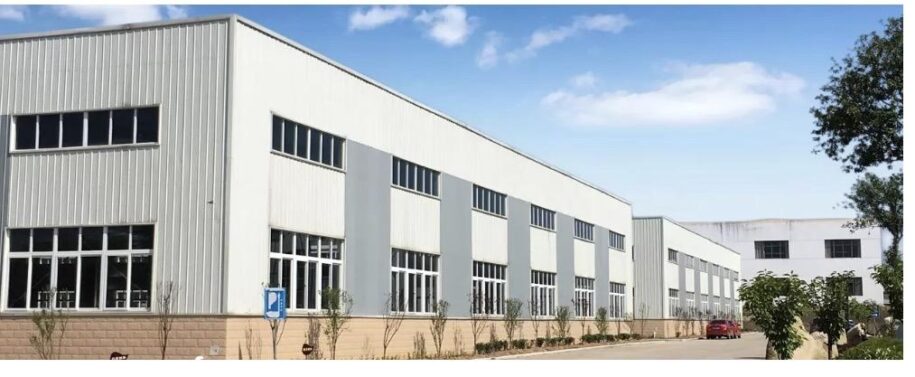
Over its 18 years of continuous operation, Bene Bags has dedicated itself to excelling in the art and engineering of tote bag design. What began as a local manufacturing enterprise in China has grown into an international B2B powerhouse, exporting premium customized bags to over 50 countries across Europe, North America, Australia, Japan, and other major global markets. This latest strategic service expansion reinforces the company’s commitment to providing versatile, eco-conscious alternatives to single-use plastics and conventional promotional items.
Navigating Global ESG Commitments and the Paradigm Shift in Retail Packaging
 The expansion of Bene Bags’ customized jute production comes at a critical juncture for international commerce. As stringent environmental, social, and governance (ESG) reporting frameworks take effect across North America and the European Union, multinational corporations and regional retailers alike are under unprecedented pressure to decarbonize their supply chains. Traditional single-use plastic bags and synthetic non-woven polypropylenes are rapidly being phased out, replaced by natural, rapidly renewable plant fibers that satisfy both regulatory compliance and heightened consumer environmental awareness.
In this shifting commercial landscape, custom tote bags have evolved from simple carryalls into strategic brand touchpoints. Modern consumers increasingly view reusable packaging as a direct reflection of a brand’s corporate ethics and environmental accountability. By expanding its manufacturing scale for raw, unbleached, and custom-dyed jute materials, Bene Bags empowers commercial enterprises to replace disposable packaging with durable, long-life promotional assets that generate thousands of organic brand impressions while actively reducing landfill waste.
Meeting Modern Brand Demands Through Diverse Material Innovations
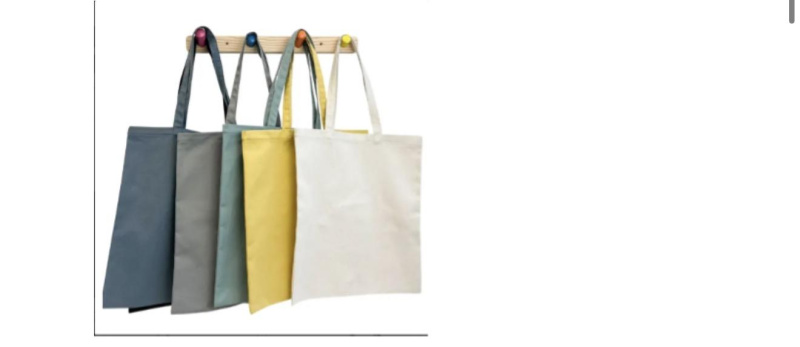
As global regulatory frameworks shift away from single-use plastics and consumers demand transparent corporate sustainability, businesses worldwide are seeking high-quality, reusable packaging that aligns with their environmental values. In response, Bene Bags is now offering its clients a broader, more sophisticated array of high-grade materials to fulfill distinct functional and aesthetic needs. Key offerings include eco-friendly jute, classic heavy-duty canvas, and lightweight yet durable Tyvek.
Each fabric option brings a distinctive appearance, texture, and technical feature to corporate identity campaigns:
- Eco-Friendly Jute Totes: Natural, biodegradable, and exceptionally strong, jute bags offer an organic, rustic texture ideal for grocery, agricultural, and eco-conscious lifestyle brands seeking to highlight green initiatives.
- Classic Canvas Totes: Sturdy, smooth, and highly versatile, high-density cotton canvas remains the gold standard for retail merchandise, trade show giveaways, and everyday urban carryalls.
- Durable Tyvek Totes: Combining lightweight agility with tear-resistant and water-repellent properties, paper-like Tyvek totes deliver a modern, industrial-chic aesthetic favored by technology firms and contemporary fashion labels.
Regardless of how unique or challenging a client’s specifications may be, Bene Bags works intimately with corporate teams to translate abstract brand requirements into finished physical products that elevate overall brand image.
Deep Technical Analysis: The Performance and Lifecycles of Next-Gen Fabrics
To assist corporate procurement teams in making data-driven decisions, Bene Bags’ engineering department has released comprehensive technical lifecycle analyses for its expanded textile line:
- The Industrial Resilience of Jute: Derived from the stem of the Corchorus plant, jute is recognized as the second most abundant natural plant fiber globally after cotton. Requiring minimal pesticide reliance and relying primarily on natural rainfall rather than energy-intensive irrigation, jute absorbs carbon dioxide at a rate significantly higher than conventional timber trees. The resulting woven fiber boasts immense tensile strength, allowing heavy-duty jute totes to carry structural loads exceeding 25 kilograms while offering 100% natural biodegradability upon end-of-life disposal.
- High-Density Cotton Canvas Craftsmanship: Utilizing heavy-weight canvas weaves ranging from 8oz to 16oz per square yard, Bene Bags constructs reinforced canvas totes featuring double-stitched stress points, bound interior seams, and heavy-duty webbing handles. Ideal for high-end retail merchandising, canvas provides an ultra-smooth printing surface that preserves fine typographic details and intricate vector graphics.
- High-Performance Tyvek Applications: Made from high-density polyethylene fibers flashed into a non-woven sheet, Tyvek offers a unique paper-like tactile feel while remaining impervious to water and virtually impossible to tear manually. Naturally recyclable, Tyvek bags appeal to tech incubators, architecture firms, and urban apparel lines looking for lightweight, minimalist, and weather-resistant packaging.
Artisanal Precision and Rigorous Quality Control Across the Production Line
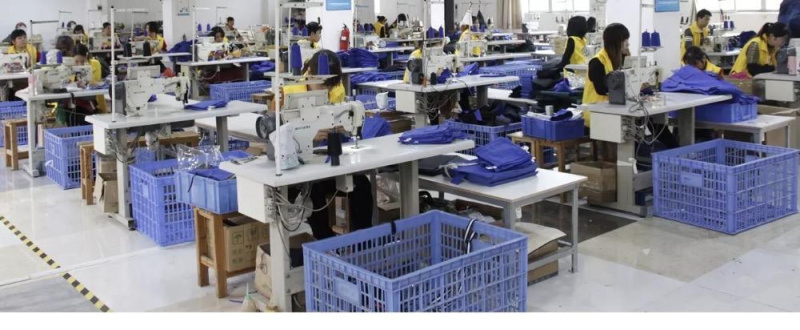
Bene Bags attributes its strong market reputation and high client retention rate to its dedicated team of industry professionals. Operating with a workforce of nearly 120 skilled personnel—spanning experienced industrial designers, master artisans, technical quality auditors, and international sales specialists—the company manages every phase of production under strict internal standards.
From raw material sourcing to final export shipping, every batch undergoes multi-stage quality inspections. The expert craftsmen at Bene Bags operate under the philosophy that perfection lies in the details. By directly controlling fabric sourcing and inspecting stitching density, handle reinforcement, and print alignment, the company ensures that first-time buyers consistently convert into long-term repeat customers.
A Philosophy of Continuous Evolution and Client-Centric Innovation
Reflecting on the milestone expansion of the jute tote bag lineup, a senior representative from Bene Bags emphasized the company’s proactive approach to manufacturing evolution:
“Though we have been in the bag manufacturing business for about 18 years, we have never ceased to evolve. Our overarching goal is to deliver uncompromised manufacturing quality while onboarding new jute fabrics and texturing options that respond directly to the diverse demands of our international clients. We pay equal attention to structural design, strap durability, and subtle customization nuances so that every client receives a product that eloquently communicates their brand story without uttering a single word.”
Streamlined Customization: Precision Color Matching and Printing Flexibility
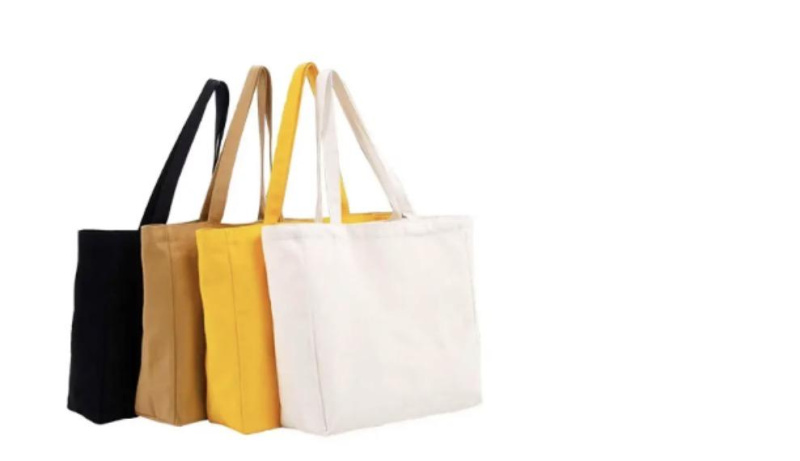
Achieving accurate brand representation across physical merchandise requires rigorous color fidelity. To support corporate brand guidelines, Bene Bags provides an extensive catalog of pre-dyed fabric colors. In cases where clients require an exact brand match outside standard stock, the tote bag manufacturer offers custom fabric dyeing services.
The ordering and customization workflow is structured for maximum transparency and ease:
- Requirements Sharing: Clients submit physical fabric samples or specify digital color references via Pantone color codes, CMYK print profiles, or RGB values.
- Sample Prototyping: The design team formulates precise dye baths and produces pre-production samples to verify color fidelity under natural lighting.
- Versatile Printing Application: Depending on the visual complexity of the client’s artwork, Bene Bags applies customized decoration techniques, including plain/unprinted natural finish, high-precision screen printing, rich embroidery, and full-color digital direct-to-garment printing.
State-of-the-Art Eco-Friendly Printing Techniques and Global Supply Chain Agility
To further complement its eco-conscious material lineup, Bene Bags has upgraded its printing facilities with water-based, azo-free pigments and REACH-compliant digital inks. Traditional solvent-based inks often release volatile organic compounds (VOCs) and create hazardous runoff during clean-up. By transitioning to non-toxic, eco-certified printing inks, Bene Bags ensures that custom logos, detailed graphics, and multi-color artwork adhere vibrant pigment to natural fibers without compromising the biodegradable integrity of the jute or canvas substrate.
Simultaneously, the manufacturer has optimized its international freight logistics network. Recognizing that retail product launches, corporate summits, and trade exhibitions operate on non-negotiable timelines, Bene Bags provides end-to-end supply chain management. From streamlined customs clearance documentation to flexible door-to-door air freight and cost-effective ocean shipping options, the company’s dedicated logistics team coordinates seamlessly with customs brokers across North America, Europe, and Australia, ensuring punctual, trouble-free deliveries.
Seamless Ordering Workflow and Online Support Infrastructure
To streamline the production pipeline and prevent artwork errors prior to mass manufacturing, Bene Bags maintains a comprehensive preparation checklist on its official web platform. The guide outlines technical prerequisites, including minimum artwork image resolution, accepted vector file formats (AI, PDF, EPS), standard color space modes, and font outline conversion guidelines.
Corporate clients, marketing agencies, and retail distributors interested in developing custom tote bags can submit detailed project inquiries directly through the company’s web portal. Bene Bags’ dedicated multilingual customer support team provides end-to-end guidance from initial material selection through sample approval, mass manufacturing, and international customs logistics.
About Bene Bags
Bene Bags is a premier custom tote bag manufacturer with 18 years of specialized expertise in delivering tailor-made eco-friendly packaging and promotional bag solutions. Operating with a professional team of 120 designers, artisans, and trade specialists, the company serves clients across 50 countries in Europe, North America, Australia, and Asia. Specializing in sustainable jute, high-density cotton canvas, and high-performance Tyvek fabrics, Bene Bags combines artisanal craft with industrial production capabilities to elevate global corporate brands.